Explore our core engineering catalog designed for strict clinical environments, lab automation, and sanitization systems.
A trusted global leader in medical device manufacturing & surgical support systems for over 30 years.
Headquartered in Shanghai, China, often referred to as the "Oriental Paris," Shanghai Emfix Medical Co., Ltd. has been at the forefront of the medical device industry for over 30 years. With a steadfast commitment to innovation and sustainable development, Emfix Medical has consistently evolved since its inception, ensuring the highest standards in research, manufacturing, and customer service.
Leveraging our decades of clinical manufacturing experience, we have successfully developed advanced Ethanol Dispenser systems to meet the highly demanding specifications of sterile hospital zones, biological cleanrooms, and automated chemical production lines worldwide. Our deep knowledge of sterile fluid control and industrial-grade mechanics allows us to deliver high-quality, corrosion-resistant, and explosion-proof sanitizing systems to global procurement managers.
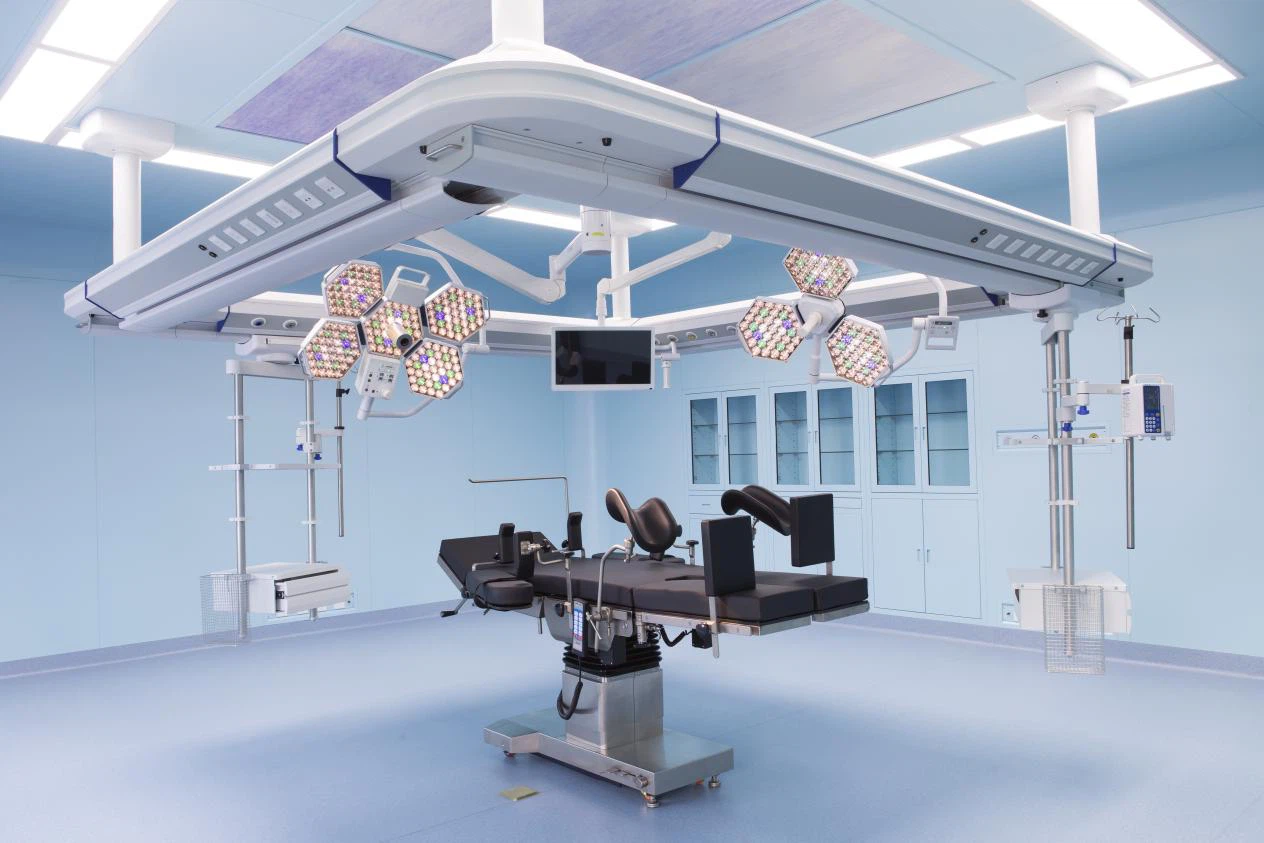
Why modern corporations require specialized, medical-grade ethanol and alcohol dispensing infrastructure.
In modern industrial facilities, microelectronics assembly plants, pharmaceutical laboratories, and health services, the demand for bulk liquid sanitization and automated ethanol delivery is rising at a compound annual growth rate. Global sourcing agents are moving away from cheap, fragile consumer-grade plastic dispensers. They now demand industrial-grade SS304/SS316 stainless steel housings, explosion-proof components for volatile fluids, and smart telemetry to minimize operation downtime.
Standardizing your supply chain with a certified China Wholesale Ethanol Dispenser Factory guarantees cost efficiency without sacrificing quality. Industrial buyers prioritize products with high duty cycles, precise volumetric calibration to prevent fluid waste, and comprehensive certification (such as CE, ATEX, and ISO frameworks) to clear stringent safety audits. Emfix Medical answers these global industry challenges by manufacturing high-yield, touchless automatic ethanol dispensing systems engineered to survive the most rigorous industrial washdowns.
Engineered for 75% to 99.9% isopropyl alcohol, ethanol, surgical spirits, and viscous sanitizing gels without pump clogging or seals degradation.
Sealed electrical compartments and intrinsically safe circuitry prevent volatile ethanol vapors from igniting, keeping industrial workplaces safe.
Micro-dosing adjustments from 0.5ml to 5.0ml reduce chemical waste by up to 40% across commercial and manufacturing operations.
Years of Medical Manufacturing Experience
Exporting Countries & Regions
State-of-the-Art Production Factories
ISO, CE, FDA, MDA Compliant
How Emfix Medical customizes fluid systems for critical sectors.
Our capabilities extend beyond manufacturing components; we provide integrated, macro-level fluid engineering solutions that fit into larger facilities' IoT systems. Whether you operate a sterile pharmaceuticals laboratory or a high-traffic manufacturing hub, our solutions are engineered for longevity and seamless assembly.
1. Automated Cleanroom Sanitization Stations: Designed for ISO Class 5 cleanrooms. Features integrated hand-sensors linked directly to cleanroom airlock doors. The doors only unlock once the personnel have initiated a complete touchless ethanol hand disinfection cycle.
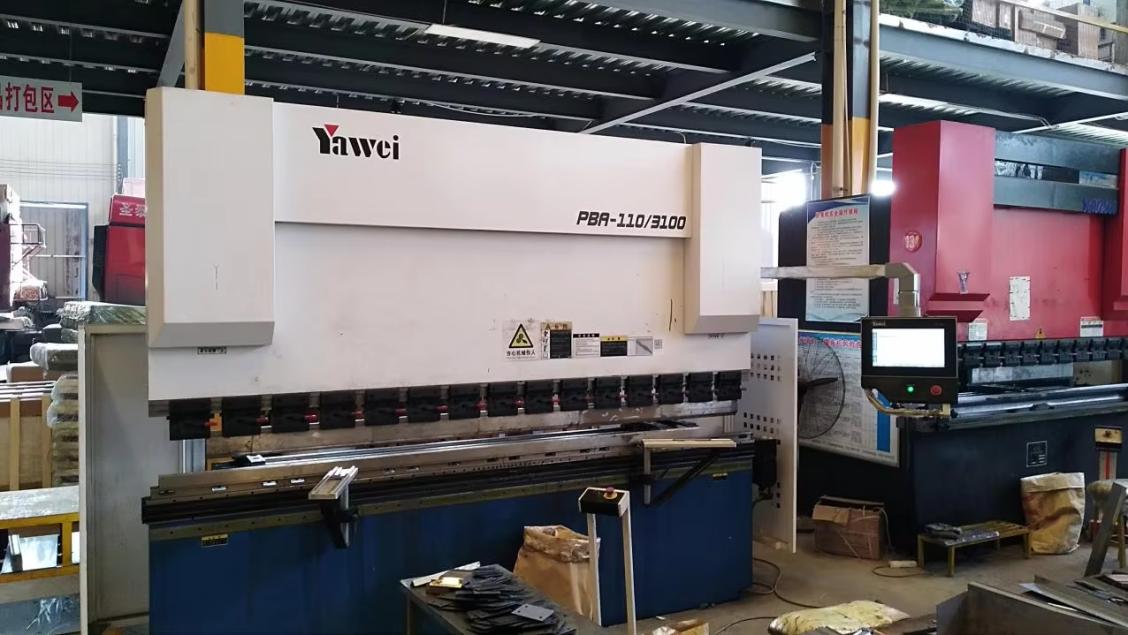
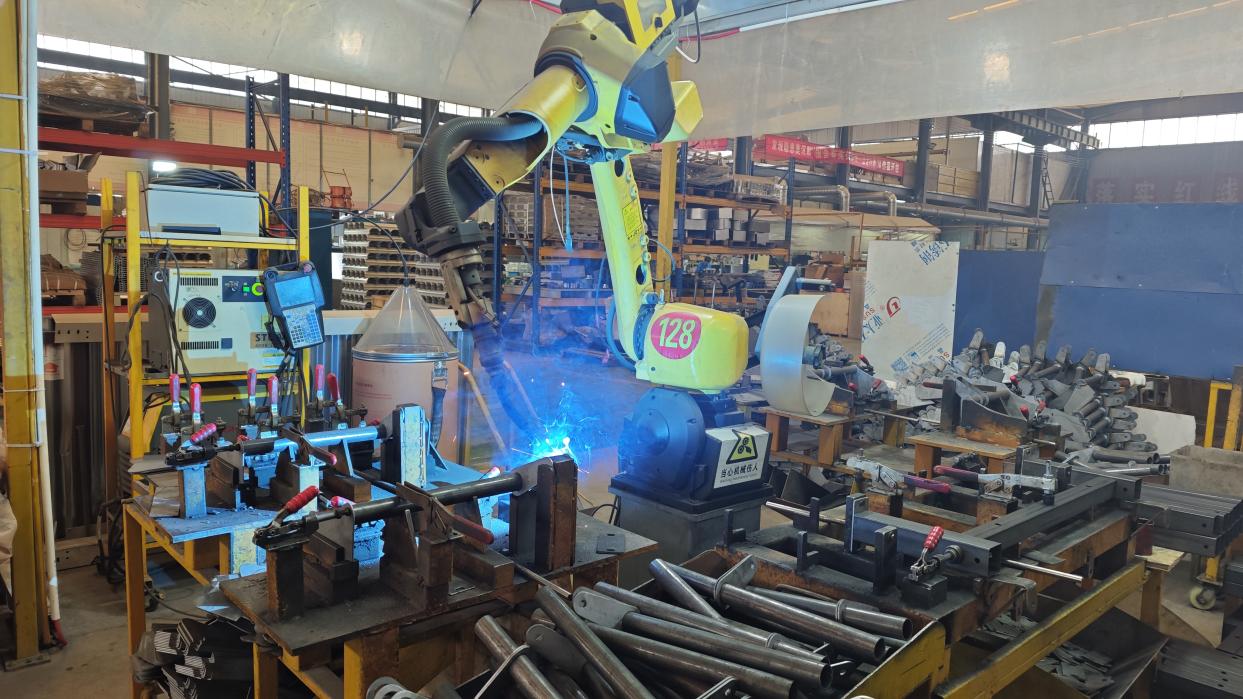
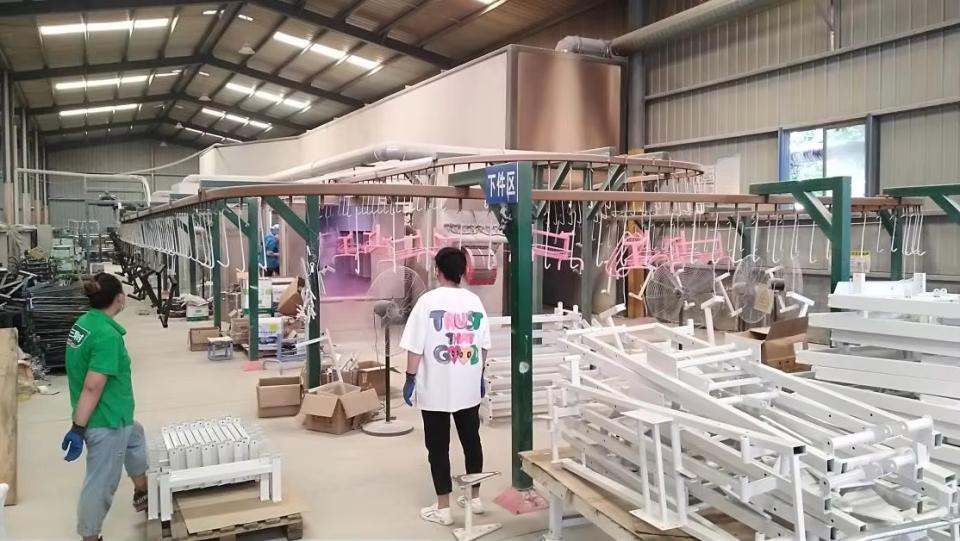
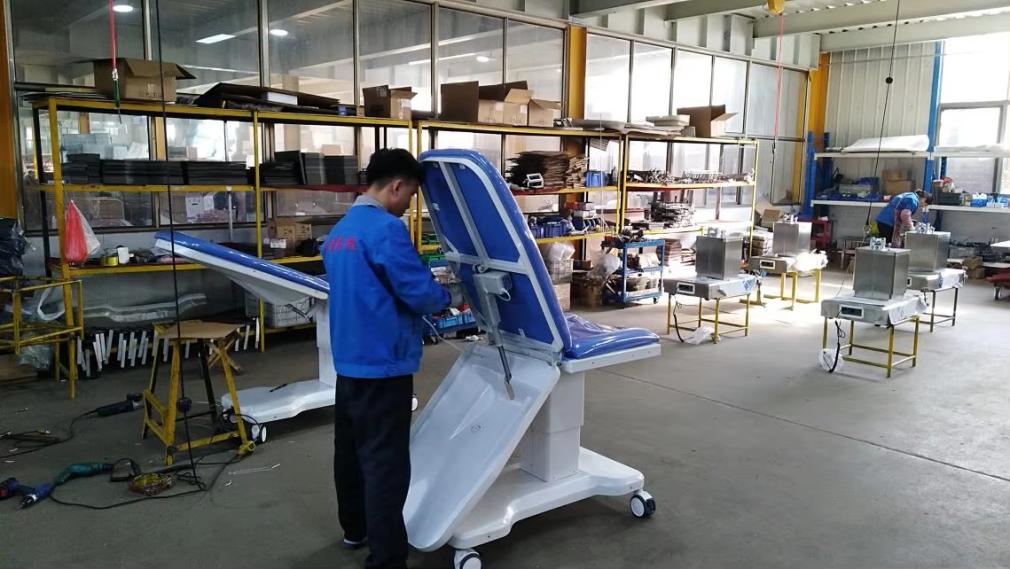
2. OEM/ODM Supply Chains for Global Brands: With 3 independent factories specializing in high-precision pipe bending, structural welding, powder coating, and electronic assembly, we assist international brands in designing, prototyping, and mass-producing private-label medical and industrial sanitizing systems.
3. Heavy-Duty Commercial & Transit Hub Infrastructure: High-traffic areas like airports, subways, and hospitals require virtually indestructible dispensers. Our stainless steel vandal-proof shells housing high-capacity 5L - 10L central reservoirs significantly lower maintenance and refill frequency.
Innovating the next generation of smart and clean liquid management systems.
Implementation of high-speed infrared motion detection with zero-latency response. Incorporates anti-interference sensor windows that prevent false triggers caused by bright surgical lamps or high-gloss industrial surfaces.
Incorporating Bluetooth & Wi-Fi modules inside the dispensers to allow facility managers to monitor fluid level, pump health, and battery levels in real-time, reducing downtime through predictive maintenance.
Developing integrated ultraviolet (UV-C) modules inside the nozzle structure to continually sterilize the dispensing area, ensuring absolute sanitary safety in surgical and pathogen-sensitive environments.
How we manufacture top-tier equipment in our three specialized factories.
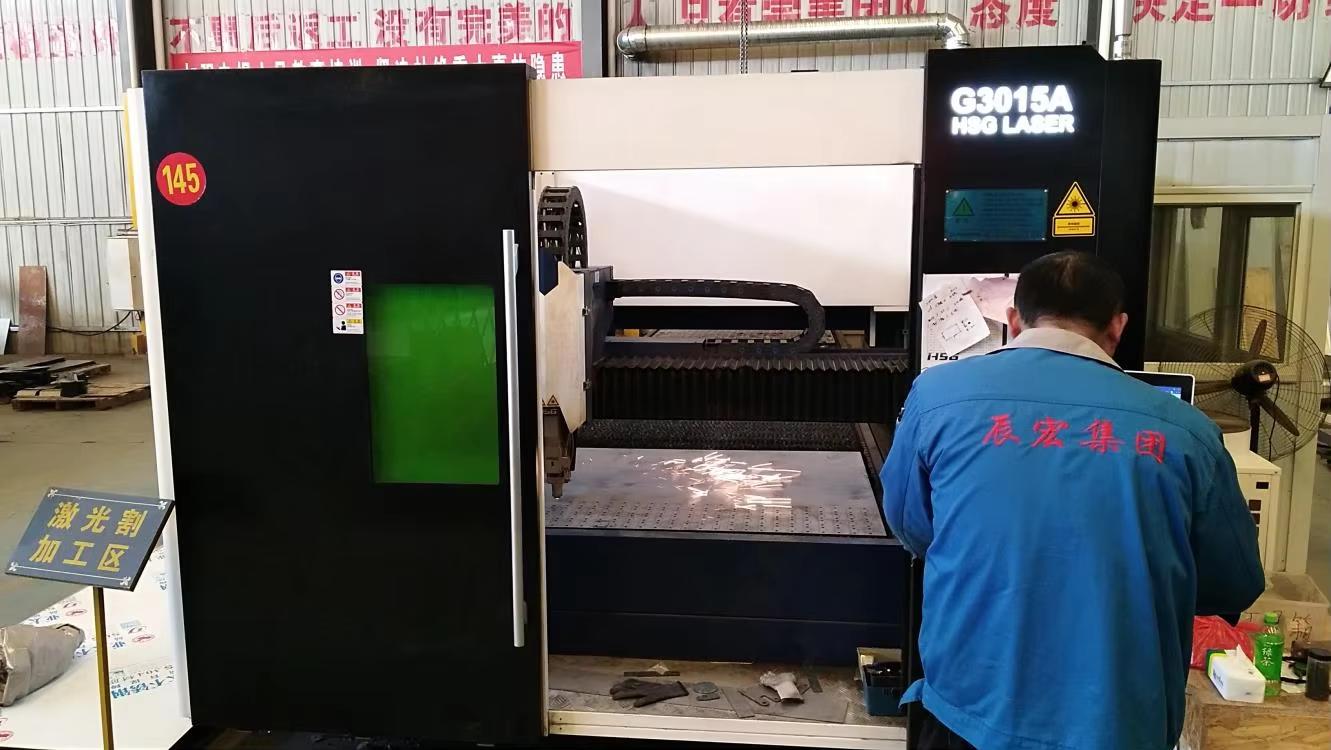
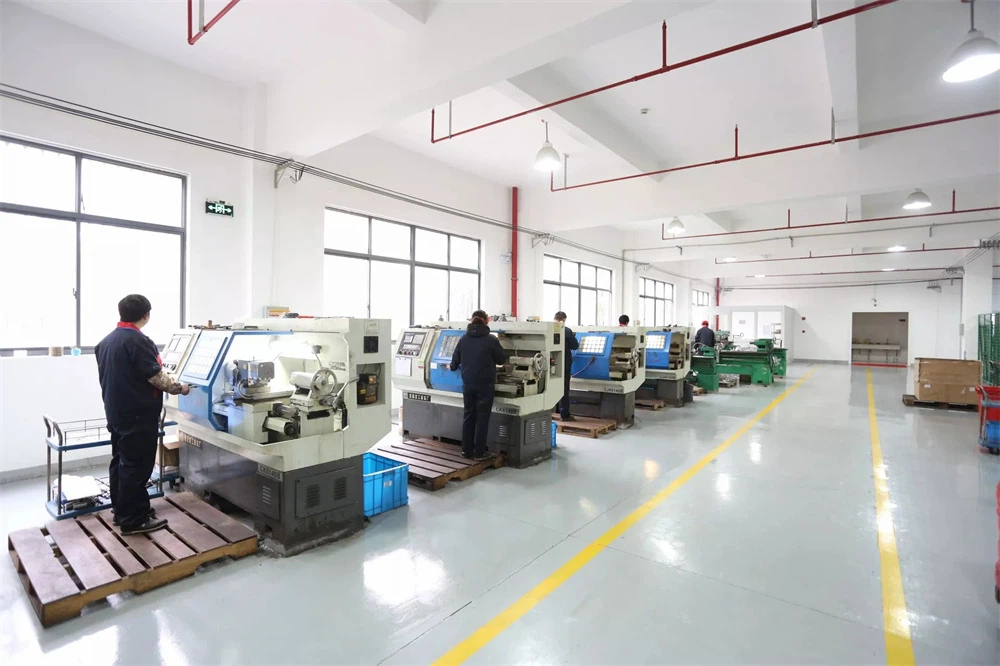
At Emfix Medical, we control every aspect of the production process with precision and dedication. We operate three state-of-the-art factories, each focusing on different product lines to ensure the highest quality across all our products. Our factories are well-organized with efficient workflows, ensuring that each production line is neat, orderly, and dedicated to excellence.
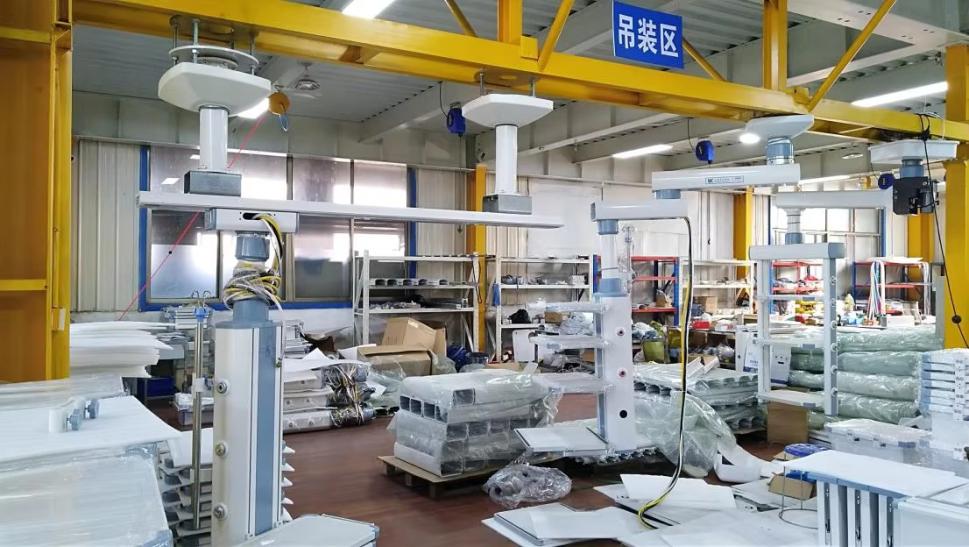
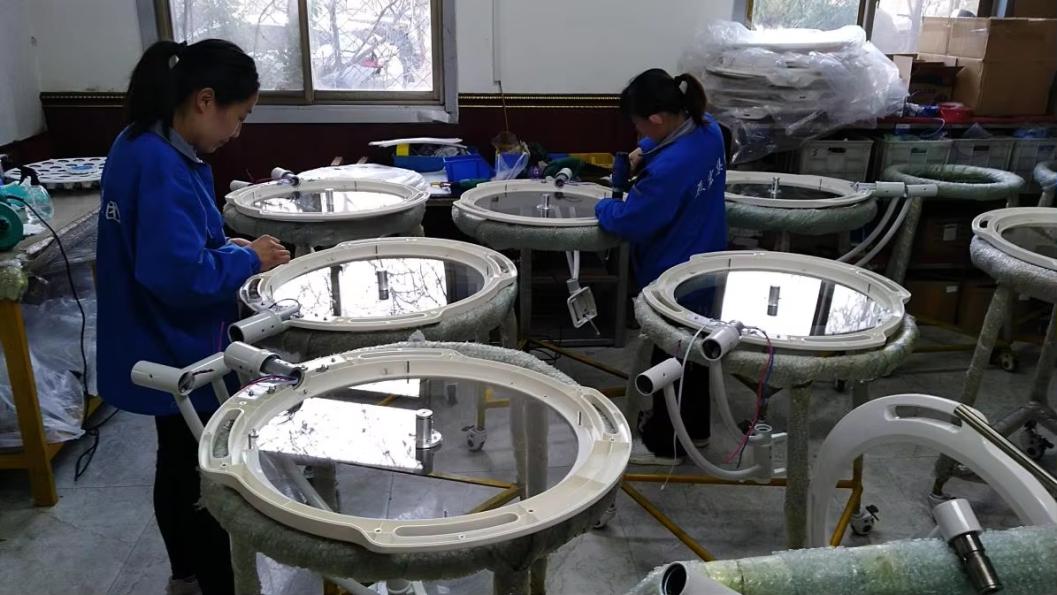
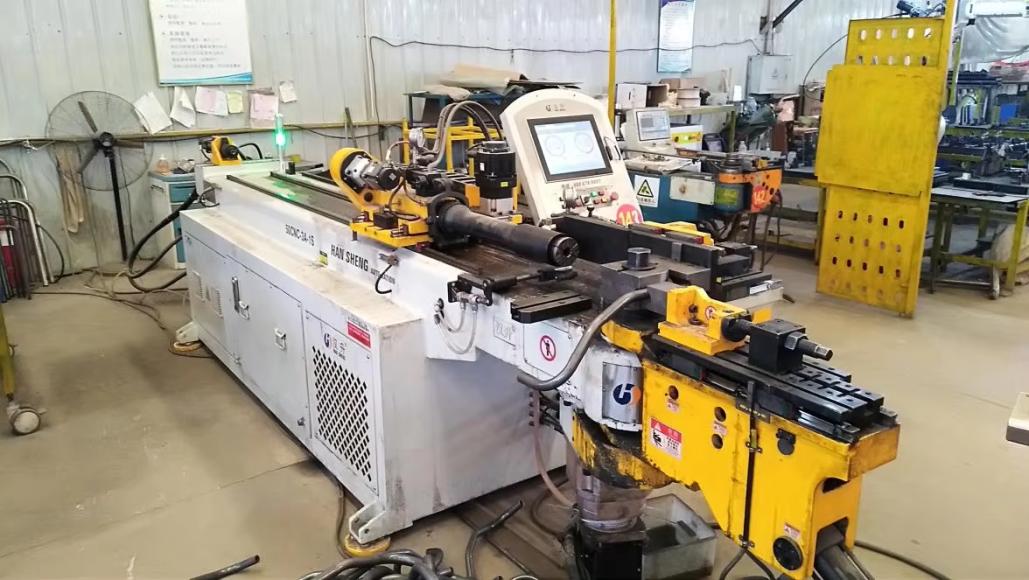
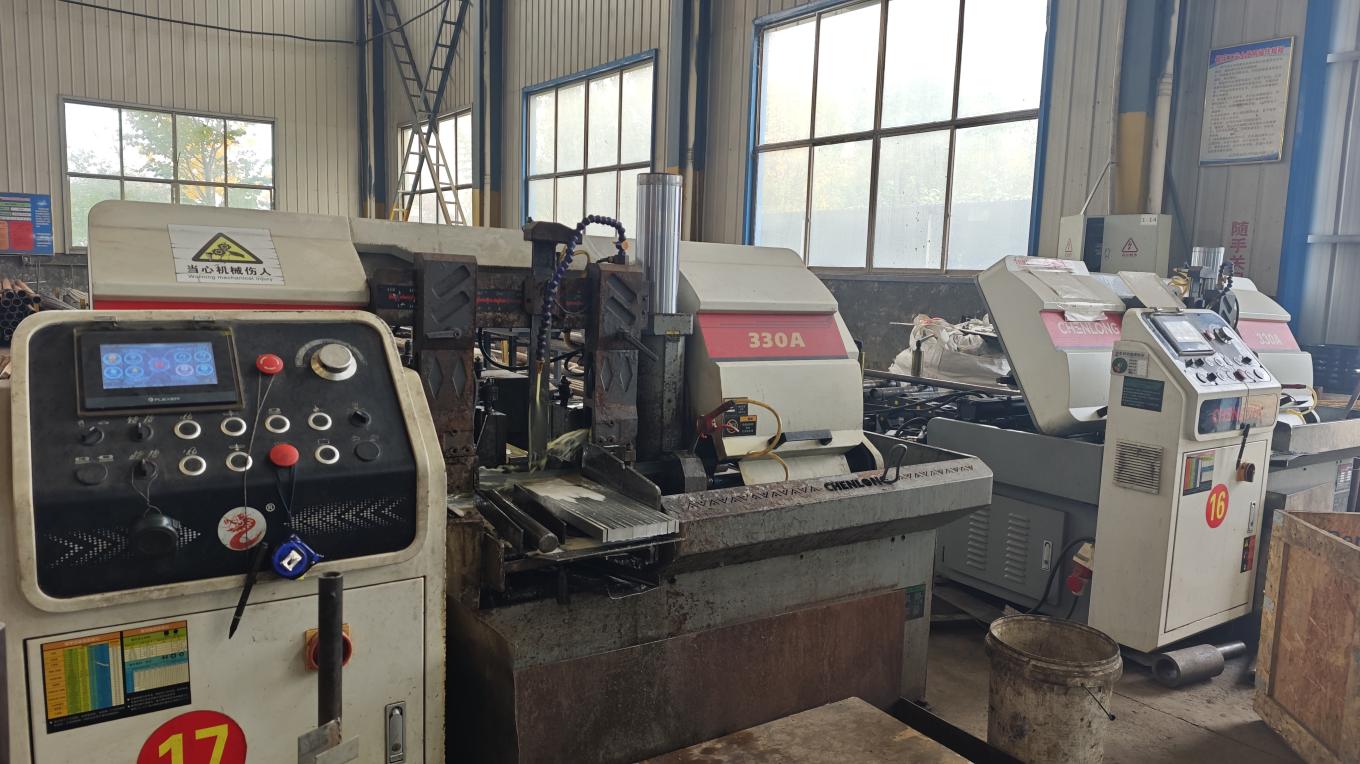
Distributing high-quality medical and fluid systems to more than 50 countries.
Emfix Medical's products are distributed in more than 50 countries across the globe, including the Asia-Pacific region, Africa, Europe, and the United States. We have cultivated an extensive network of distributors and technical partners, enabling us to continually expand our market reach and promote the Emfix brand internationally.
We are actively engaged in technical collaborations with leading organizations in Europe, the United States, and other international markets, ensuring we stay ahead in terms of product development and technological advancements. By merging localized customer support with our robust Chinese manufacturing base, we offer seamless customs coordination, rapid shipment logistics, and on-site engineering consultations for high-volume purchasers.
If you're looking for reliable, high-quality medical equipment that meets international standards, look no further than Shanghai Emfix Medical Co., Ltd. Join our growing network of healthcare providers and distributors and experience the difference of working with a leader in the medical device industry.
Contact Sourcing DirectorDirect technical answers to help purchasing managers make informed decisions.
Our standard Minimum Order Quantity (MOQ) for custom-branded or wholesale ethanol dispensers is typically 100 units. However, for specialized medical projects or introductory trials, we can accommodate lower quantities. Contact our sales department to discuss custom tooling or private labeling requirements.
Yes. Our ethanol dispensers designed for industrial cleanrooms utilize explosion-proof electronics and encapsulated battery cases. Ethanol has a flashpoint of approximately 13°C (55°F) in standard mixtures. Therefore, our design eliminates static electricity risks, open sparking, and thermal overheating.
Shanghai Emfix Medical is ISO 13485 certified for medical device production. Our products carry CE marks, FDA registrations, and MDA compliance, ensuring hassle-free imports and local safety compliance in EU, US, and Southeast Asian markets.
We use premium fluorine-rubber (Viton) gaskets and medical-grade silicone tubing. These materials resist structural swelling and degradation caused by high-concentration ethanol. Additionally, the pump head mechanisms are isolated from direct motor heat, reducing maintenance downtime.
Absolutely. We possess full metal fabrication tooling (Pipe Bending, Laser Cutting, CNC Welding, and automated Powder Coating). We can customize dimensions, shell materials, brand logos, mounting brackets, and supply-voltage configurations to integrate with your existing infrastructure.
Standard orders are completed within 30 to 45 business days. Highly customized OEM dispenser orders requiring custom molds may take 60 days. We export directly out of Shanghai Port, offering highly competitive maritime shipping times globally.
Explore our highly specialized surgical suite systems, digital integration tools, and ICU monitoring devices.
 Emfix Medical